Custom Rigid Set Up Boxes Wholesale for Pharmaceutical Packaging
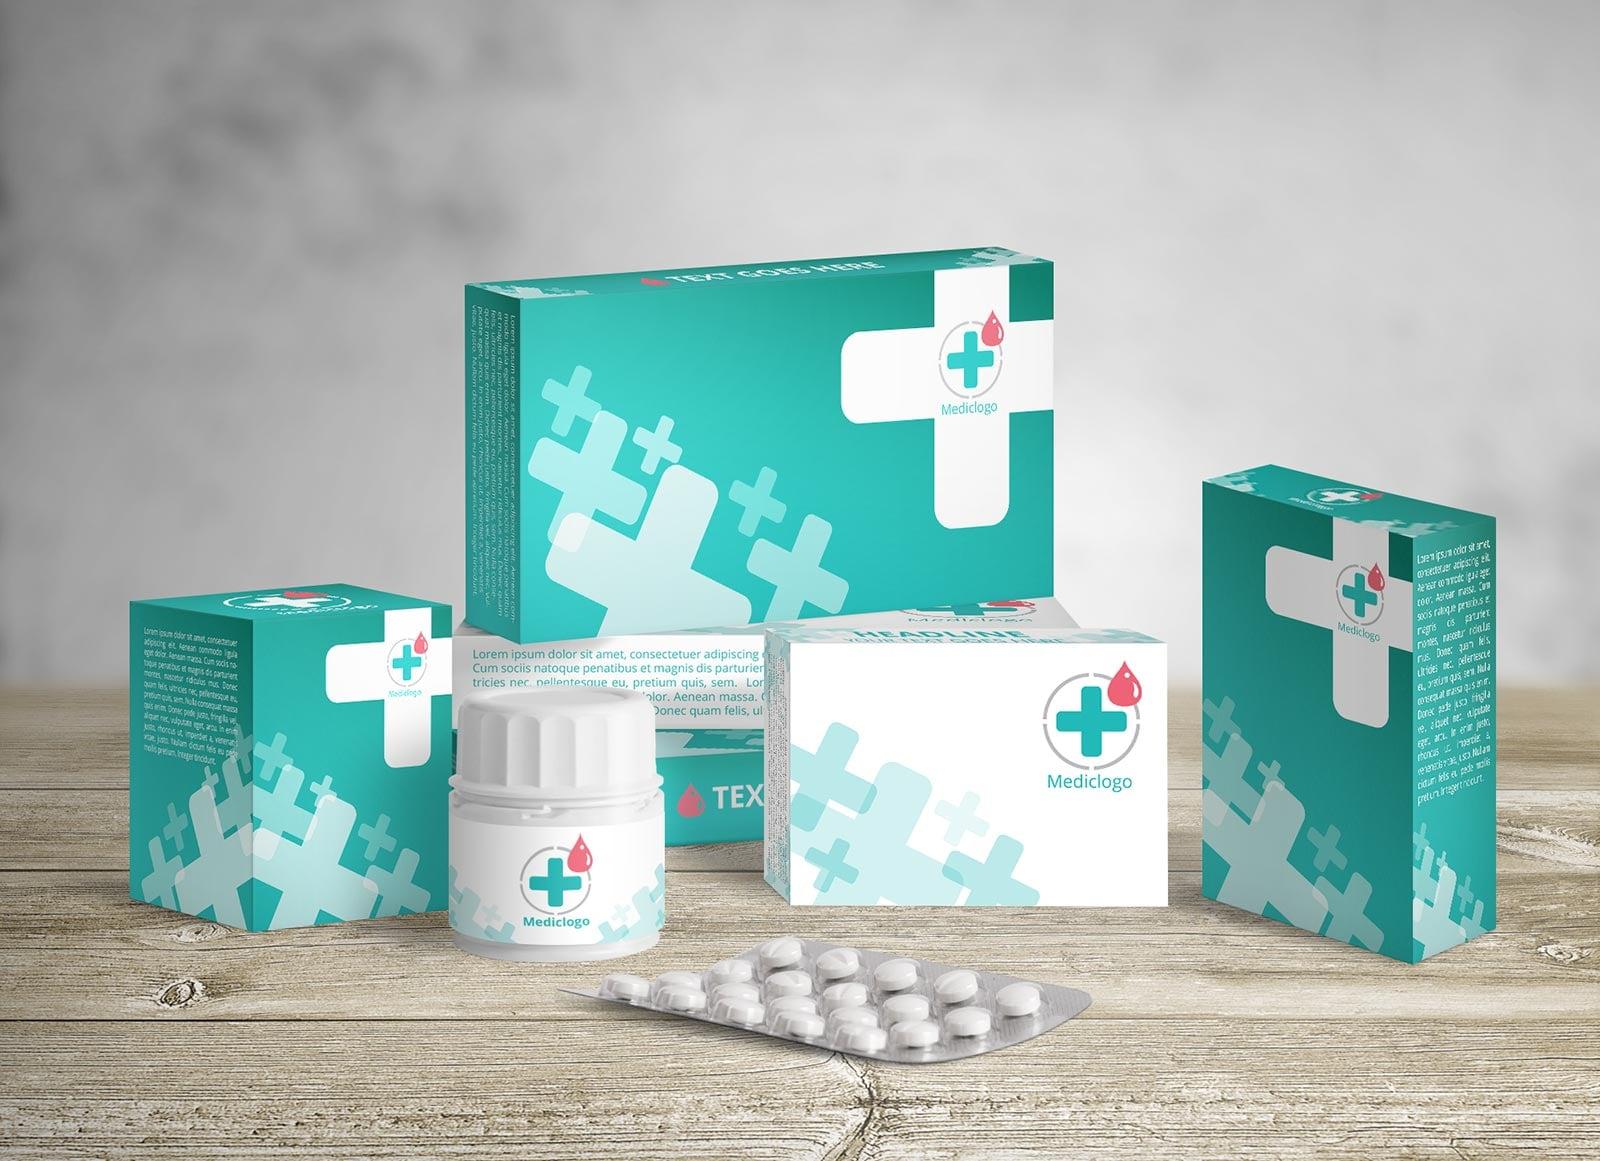
How Custom Rigid Set Up Boxes Wholesale Support Pharmaceutical Packaging
Pharmaceutical packaging must protect products, preserve their quality, and communicate accurate information throughout storage and distribution. Wholesale rigid boxes can provide a sturdy secondary packaging structure for suitable medicines and healthcare products, but the complete packaging system must meet applicable safety, labeling, and regulatory requirements.
Why Pharmaceutical Packaging Matters
Pharmaceutical packaging is more than an outer container. It supports product protection, identification, traceability, and safe handling. Poorly selected packaging can expose products to damage, create labeling confusion, or make storage and transportation more difficult.
Rigid boxes are made from thick paperboard and retain their shape under normal handling. They can be suitable for selected healthcare gift sets, medical device accessories, promotional kits, and secondary packaging applications where permitted.
Businesses considering custom rigid set up boxes wholesale should first identify the product's storage requirements, sensitivity to environmental conditions, and intended distribution channels. The packaging must be appropriate for the specific product rather than selected on appearance alone.
Selecting Packaging for Different Pharmaceutical Products
Different pharmaceutical products require different packaging structures. Tablets, bottles, medical devices, and healthcare kits may need different levels of protection and internal organization.
Packaging for Bottles and Healthcare Products
Bottled products may require secure compartments that limit movement during handling. Inserts can help hold containers in place, while appropriately designed outer boxes provide additional structure.
Custom Pharmaceutical Packaging Boxes can accommodate bottles, instruction leaflets, and other permitted components. However, the primary container must provide any necessary moisture, light, or contamination protection. A paperboard box alone should not be assumed to provide a suitable barrier.
Packaging for Tablets and Capsules
Tablets and capsules commonly rely on primary packaging such as blister packs or appropriately designed bottles. The outer carton provides space for product identification, instructions, and required labeling.
A rigid outer box may be suitable for certain secondary packaging applications, but it should not replace the validated primary packaging system. Businesses should confirm that the complete arrangement protects product quality and supports the required storage conditions.
Packaging for Medical Devices and Healthcare Kits
Some medical devices and healthcare kits contain multiple components that must remain organized during storage and transportation. Custom inserts can separate components, reduce movement, and make the contents easier to identify.
When ordering custom rigid set up boxes wholesale, businesses should assess the complete package, including internal supports, protective wrapping, and shipping cartons. Any sterile medical device must retain the integrity of its validated sterile barrier system.
Essential Features to Consider Before Ordering
Selecting pharmaceutical packaging requires careful attention to materials, dimensions, labeling, and product compatibility.
Material Quality and Product Protection
The appropriate packaging material depends on the product's sensitivity to moisture, light, oxygen, and physical damage. Some products require specialized barrier materials, while others may be adequately protected by a suitable primary container and secondary carton.
Paperboard strength should match the expected handling conditions. Businesses should also verify that inks, coatings, adhesives, and inserts are appropriate for their intended use and do not compromise product safety.
Dimensions and Internal Inserts
Accurate dimensions help keep products secure and improve packing efficiency. Measurements should account for the primary container, protective components, and any accompanying documentation.
Custom Pharmaceutical Packaging Boxes can include fitted inserts or partitions for suitable applications. These features can improve organization, but the design must not interfere with essential labeling, container access, or required safety features.
Labeling, Traceability, and Tamper Evidence
Pharmaceutical labels must be readable, accurate, and positioned appropriately. Depending on the product and jurisdiction, required information may include the product name, strength, dosage instructions, ingredients, expiration date, batch or lot number, and other regulatory details.
The US Food and Drug Administration provides guidance on container and carton labeling intended to help minimize medication errors. Its recommendations address the presentation of critical information so users can identify and use medicines correctly. .
Certain medicines also require tamper-evident features. The FDA explains that covered over-the-counter drug products must use packaging designed to provide visible evidence if tampering occurs. A decorative rigid box does not automatically satisfy this requirement. .
Wholesale Ordering and Cost Management
Wholesale purchasing can reduce unit costs, but the total value depends on material specifications, manufacturing quality, shipping, storage, and order quantities.
Request Samples and Confirm Specifications
A physical sample helps buyers inspect dimensions, construction, closure quality, and print accuracy. It also allows teams to confirm that products fit correctly and that the package can be assembled efficiently.
Before placing an order for custom rigid set up boxes wholesale, request a written quotation covering setup fees, minimum order quantities, material options, production timelines, and delivery charges.
For regulated pharmaceutical products, packaging changes should also be reviewed through the appropriate quality and regulatory processes before production approval.
Plan Inventory and Production Carefully
Large orders may lower the unit price, but they can increase storage expenses and the risk of obsolete packaging if product information changes.
Businesses should consider forecast demand, product shelf life, labeling updates, and production schedules. Accurate inventory planning helps prevent shortages while reducing excess printed packaging.
Sustainability and Quality Control
Businesses can explore responsibly sourced paperboard, recycled-content materials, and designs that reduce unnecessary packaging. These options should be evaluated against the product's protection requirements and applicable regulations.
The World Health Organization's good manufacturing practices for pharmaceutical products emphasize controlled production processes and quality assurance. Packaging materials and operations should therefore be managed through appropriate supplier qualification, specifications, inspections, and documentation.
Custom Pharmaceutical Packaging Boxes should undergo relevant quality checks before release. These may include verifying dimensions, checking print accuracy, confirming label information, and assessing whether the packaging meets approved specifications.
Environmental claims should also be verified. Recyclability depends on the complete material combination, coatings, adhesives, and local recycling infrastructure.
Frequently Asked Questions
Are rigid boxes suitable for all pharmaceutical products?
No. They may be suitable as secondary packaging for selected products, but medicines and sterile devices can require specialized primary containers, validated barriers, or specific tamper-evident features.
How can pharmaceutical businesses reduce packaging costs?
Compare suppliers, standardize compatible dimensions, request samples, and plan order quantities around demand. Any cost-saving change must preserve approved specifications and product protection.
What should be checked before pharmaceutical packaging production?
Verify material specifications, dimensions, labeling accuracy, traceability requirements, and applicable safety features. Required quality and regulatory reviews should be completed before production approval.
Final Thoughts
Pharmaceutical packaging combines product protection, clear communication, quality control, and regulatory compliance. Businesses should evaluate the complete packaging system before choosing materials, inserts, or decorative finishes.
By comparing suppliers, validating samples, and managing inventory carefully, businesses can use custom rigid set up boxes wholesale for appropriate secondary packaging applications. The best solution supports product integrity and efficient distribution while meeting the requirements of the relevant market.

 English
 Arabic
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek